A mould built to your drawings and to the standards named in your RFQ — not a catalogue tool adapted to your part. Send 2D/3D drawings, a material target and the annual volume, and engineering feedback plus a quotation come back within 24 hours.
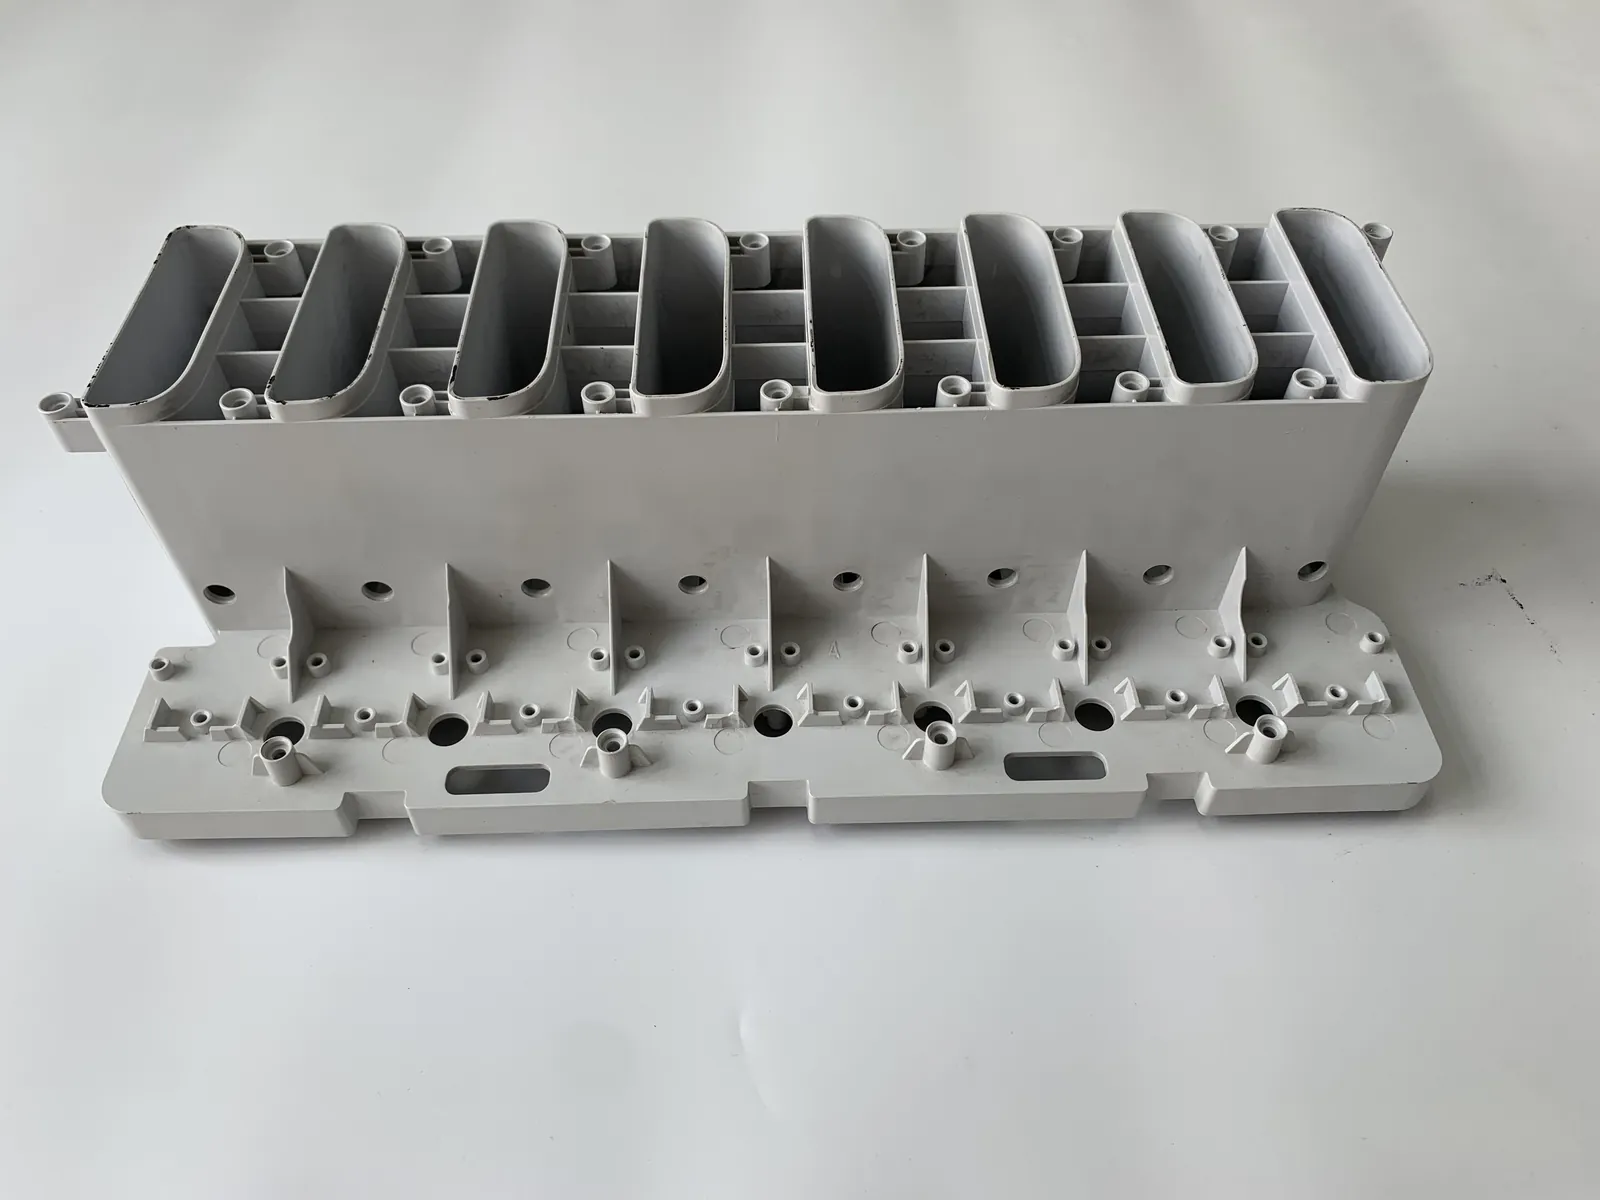
Tool types
- Single and multi-cavity injection moulds for parts of small to medium complexity, with ejection, cooling and runner layouts chosen per part
- Automotive interior and exterior component moulds built against customer part-approval workflows, with dimensional reports and trial documentation to match
- High-precision moulds for medical device components and consumer electronics housings
- Two-shot (2K) tooling that bonds two materials in one cycle
- Hot runner manifolds that remove runner scrap
- Stack tooling for thin walls at high cavity counts
- Export moulds prepared for shipment and commissioning at the customer site
How the build is controlled
Design and inspection follow the standards you specify in the RFQ. Standard and hardened mould steels are selected per part and lifetime target, and the quotation names the steel grades and the component suppliers, so nothing shifts between what you approve and what gets built.
The build sequence is fixed and agreed up front: RFQ and drawing review, DFM and quotation, tool design, steel ordering and machining, fitting and assembly, trials and sampling, shipment.
Which tool type fits your program?
| Tool type | Typical use |
|---|---|
| Single-cavity | Low-volume programs or large parts |
| Multi-cavity | Higher annual volumes on one part family |
| Two-shot (2K) | Multi-material parts molded in one cycle |
| Hot runner | Runner-less production with less scrap |
| Stack | Thin-wall, high-cavity programs |
| Export mould | Shipment and commissioning at the customer site |
What do we need from you to quote a mould?
2D/3D drawings, a material target and the annual volume. A quotation follows within 24 hours; bigger or multi-cavity work carries its own schedule, agreed with you and written into that quotation.
Lead time
Around 45 days is typical for a small tool. Larger and multi-cavity projects are planned one at a time, with the schedule set out in the quotation.
After the tool is built
Customer moulds stay with us for storage, maintenance and servicing between runs. When parts are needed, the tool is matched to a machine on a floor of 11 presses covering 80 to 450 tons, and every batch keeps its process record so a repeat order can be reproduced.
Related: injection molding services, and the field note on how a 45-day tooling timeline is built.
Send your drawings and requirements — DFM feedback and a quotation within 24 hours. Use the WhatsApp button on any page or the contact page.
How we compare with typical US/EU tooling suppliers
Cost and lead-time figures below are industry-typical. Your actual saving is confirmed per project after DFM.
| Hongqiang Mould | Typical US/EU tooling suppliers | |
|---|---|---|
| Quote turnaround | Within 24 hours of your 2D/3D drawings | Often several business days |
| Production chain | 11 presses (80–450 T) + 5 CNC + EDM, wire-cut, grinding, fitting + CMM — full in-house toolmaking | Often outsources part of the process |
| Communication | Direct WhatsApp / email to engineers | Time zones + multiple subcontracting layers |
| Pricing | Quoted per project — send your local quote and we benchmark like-for-like (same steel, same cavity spec) | Local premium rates |
| Inspection | Every mould through the CMM room | Varies by supplier |
Frequently asked questions
How fast can I get a quote?
Within 24 hours after we receive your 2D/3D drawings.
Do you make molds in-house?
Yes. 11 injection presses (80–450 T), 5 CNC machines plus EDM, wire-cut EDM, grinding and fitting, and a CMM inspection room. Full toolmaking is done in-house.
How do you control mold quality?
Every mold goes through our CMM inspection room, and toolmaking (CNC, EDM, wire-cut, grinding) is done in-house so tolerances stay under our control.
From Bridge Tooling to Volume Production — One Toolroom
Early samples, bridge tooling and volume runs usually get split across three different suppliers. At Hongqiang they stay under one roof. The toolroom that cuts your first bridge tool is the same one that runs it later on the floor, across 11 injection presses from 80 to 450 T, supported by 5 CNC machines plus EDM, wire cutting and grinding in-house. Nothing gets re-quoted or re-tooled somewhere else when your part moves from first shots to repeatable production.
- Bridge tooling built in the same toolroom that will later run production
- 11 presses (80–450 T) covering pilot samples through volume runs
- 5 CNC plus EDM, wire cutting and grinding kept in-house
- Every tool qualified in our own CMM inspection room before it leaves
Send your 2D/3D drawings and we return a quote within 24 hours. Lead times and volumes are confirmed per project after DFM.